Dual-Energy X-Ray Inspection Systems
Dual-Energy X-Ray Inspection Systems utilize advanced multi-spectrum X-ray technology to detect challenging low-density contaminants that may be difficult to identify using conventional inspection methods. By combining Dual-Energy imaging, Time Delay Integration (TDI), and AI-powered inspection algorithms, these systems deliver enhanced contaminant detection, reduced false rejects, and improved product quality across a wide range of food processing applications.
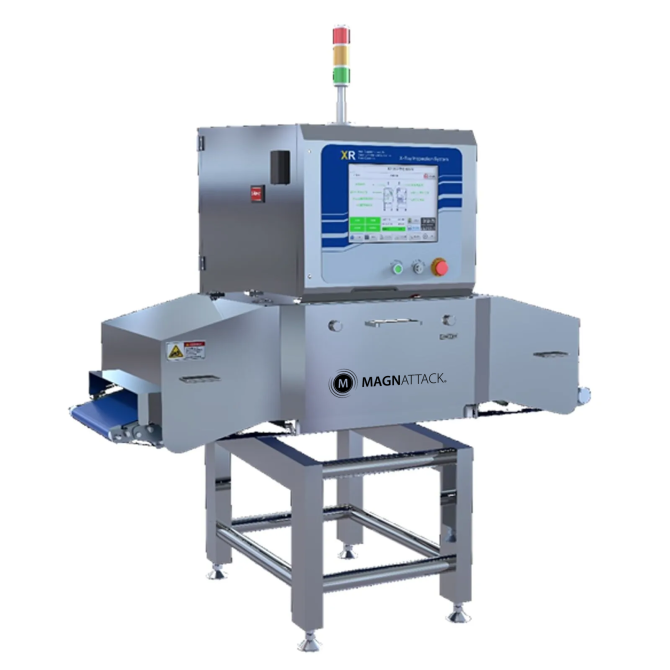
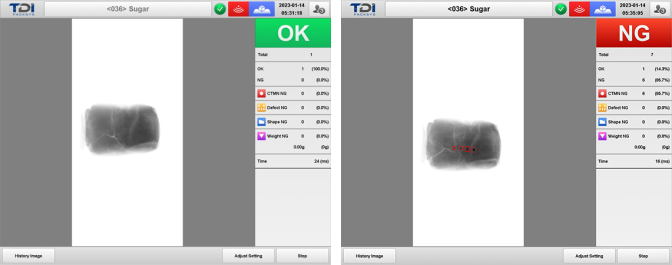


Overview
Time Delay Integration (TDI)
Time Delay Integration (TDI) is an advanced imaging technology designed to improve X-ray detection accuracy and image quality. TDI works by combining multiple rows of surface images into a single high-resolution line image through signal accumulation, resulting in greater image clarity and enhanced contaminant detection performance.
The system features an 8-stage TDI detector, providing up to 8 times more detector exposure than a standard linear array detector using the same X-ray energy. This increased exposure produces clearer images, improved sensitivity, and more reliable detection of foreign materials and product defects.
Dual-Energy Technology
Dual-Energy X-Ray Inspection combines advanced Time Delay Integration (TDI) imaging with Dual-Energy X-Ray Inspection to deliver enhanced foreign material detection. By utilizing two different X-ray energy levels, the system analyzes how materials absorb energy across multiple spectrums and compares the results to identify differences in material composition. This enables detection based not only on density, but also on material characteristics.
This technology helps identify low-density contaminants that may be difficult for conventional X-ray systems to detect, including:
- Bone
- PVC
- Thin glass
- Soft metals such as aluminum
By overcoming many of the limitations of traditional detectors, Dual-Energy technology improves detection accuracy, reduces false rejects, and enhances contaminant detection performance in meat, poultry, dairy, and processed food applications.
Smart Algorithms (AI)
Smart Algorithms (AI) provide an additional layer of inspection by enabling the system to simulate computer vision and optically inspect X-ray images for contaminants. If a contaminant can be visually identified within the X-ray image, it can be detected even when its density is too low for traditional X-ray algorithms to identify. Smart Algorithms are developed on a product-by-product and application-specific basis, allowing the system to learn the normal appearance of each product and identify visible contaminants, defects, and irregularities regardless of density. This technology can also be utilized in specialized applications, including the detection of oil in seals, which has a density less than water.
Features
- Dual-Energy X-ray technology uses multiple X-ray energy levels to improve detection of low-density contaminants and challenging foreign materials.
- Time Delay Integration (TDI) imaging technology increases image clarity through increased detector exposure, resulting in clearer visuals and significantly improved contaminant detection.
- AI-powered inspection algorithms identify low-density contaminants, organic foreign materials, and product quality defects.
- Comprehensive contaminant detection identifies metallic and non-metallic contaminants, including glass, stone, bone, ceramic, rubber, and plastic.
- Enhanced low-density contaminant detection supports the identification of chicken bones, soft plastics, rubber fragments, PVC, thin glass, and other difficult-to-detect materials.
- Ultra-sensitive inspection performance detects stainless steel particles down to 0.3 mm and ferrous wire as small as 0.2 mm x 2 mm.
- Automated rejection capabilities remove suspect products without interrupting production when paired with suitable rejection systems.
- Defect and packaging integrity inspection helps identify missing components, breakage, misalignment, and other product quality issues.
- Optimized product flow with German-engineered conveyor belting helps maintain consistent inspection alignment and minimized product drift
- Industrial-grade computing power supports fast image analysis and real-time algorithm processing, ensuring speed and reliability in high-throughput food manufacturing x-ray machines.
- Customizable programming allows generator strength, speed, and sensitivity settings to be tailored to specific products and applications.
- User-friendly Windows-based interface provides access to real-time product imaging, inspection data, and program management.
- Real-time data logging and reporting support production monitoring, traceability, and audit requirements.
- Remote diagnostics and technical support capabilities help maximize system uptime and operational performance.
- Secure user access controls help protect inspection settings and prevent unauthorized changes.
- Hygienic stainless steel construction with IP66-rated 24V DC brushless motors for smooth, contamination-resistant operation in washdown environments. Optional IP69K washdown capability is available for sanitary food production environments.
- Built with proven industrial components from leading suppliers, including VJT, Siemens, and Schneider, for long-term reliability and performance.
- Inspects a wide range of products, including bulk, vacuum-sealed, tray-packed, or boxed.
Applications
- Chicken bone detection in boneless thighs, breasts, and tenders
- Poultry inspection involving overlapping or irregularly shaped products
- Meat and protein processing applications
- Sliced, shredded and block dairy and cheese products
- Packaged food inspection, including trays, pouches, and vacuum-sealed products
- Snack foods and convenience products
- Frozen meals and prepared foods
- High-speed food manufacturing environments requiring advanced foreign material detection
DUAL-ENERGY X-RAY INSPECTION SYSTEMS
| XR-4080SDE | XR-6080SDE | |
|---|---|---|
| Description: | XR-SDE Dual Energy X-Ray | XR-SDE Dual Energy X-Ray |
| X-Ray Generator: | MAX 80kV, 350W | MAX 80kV, 350W |
| Inspection Width: | 400 mm | 600 mm |
| Inspection Height: | 220 mm | 300 mm |
| Conveyor Speed: | 10-60m/min | 10-60m/min |
| Operating System: | Windows Professional | Windows Professional |
| X-Ray Emissions: | < 1 μSv/h (CE standard) | < 1 μSv/h (CE standard) |
| IP Rating: | IP69K | IP69K |
| Working Environment: | Temperature: 32-104°F; Humidity: 30-85% (no dew) | Temperature: 32-104°F; Humidity: 30-85% (no dew) |
| Reject Options: | Sound and Light Alarm; Belt Stop; Optional Rejectors | Sound and Light Alarm; Belt Stop; Optional Rejectors |
| Power Supply: | 220V/60Hz | 220V/60Hz |
| Construction: | Stainless 304 | Stainless 304 |
| Operator Interface: | 15″ Touchscreen HMI | 15″ Touchscreen HMI |
| Data Export: | USB/Ethernet | USB/Ethernet |
| Finish: | Mirror Polish / Bead-Blasted | Mirror Polish / Bead-Blasted |
Note: Product models and specifications are subject to change. For more information, contact Magnattack
Powered by TDI
Talk to an Expert
Got a question or need a quote? Our Magnattack experts are here to offer fast, personalized guidance for all your magnetic separation needs.
Contact us today and experience the reliability and responsiveness that sets us apart in supporting your success.
United States
(630) 994-3310
Australia & International
+61 2 4272 5527
New Zealand
099 424 897
South America
+54 9 2352 44-9007